×

2026 Top Micro Drill Hard Coating Machine Suppliers

A micro-drill can be thinner than a human hair, yet its cutting edges must survive heat, friction, and repeated contact with hard materials. That makes the Micro-Drill Hard Coating Machine more than a finishing tool. It is part of a controlled process involving substrate preparation, coating uniformity, temperature, and inspection. Small details matter.

SEMI reported that global semiconductor manufacturing equipment sales reached US$117.1 billion in 2024. This figure is not a measure of micro-drill coating demand. It does, however, show the scale of investment in a sector where precision tooling supports demanding production processes. Buyers should compare suppliers on verifiable machine capabilities, process repeatability, service access, and sample results—not headline specifications alone.

Quality pioneer W. Edwards Deming is widely associated with the reminder, “In God we trust; all others must bring data.” For supplier evaluation, that means asking for coating-thickness records, documented test conditions, and evidence from drills similar to your own. No single coating wins everywhere. A machine suited to one drill diameter or substrate may perform differently on another. That is easy to overlook.

This 2026 supplier guide focuses on practical questions: what each system can coat, how consistently it runs, and what support follows installation. Published industry reports rarely isolate this niche, so precise market-size claims deserve caution. Request a sample run. Inspect the edges under magnification. Then compare the results against your actual production needs.
2026 Top Micro Drill Hard Coating Machine Suppliers

What Micro Drill Hard Coating Machines Are

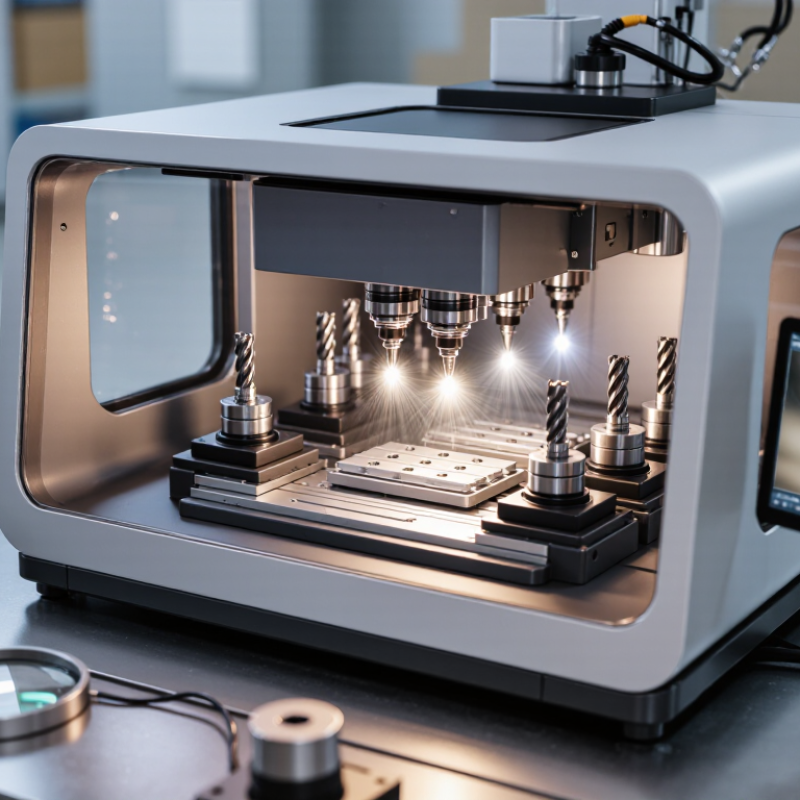
A micro drill hard coating machine is a vacuum system that deposits a thin, wear-resistant layer onto small cutting tools. It is not a drill grinder. The system typically includes a vacuum chamber, a heating stage, coating sources, gas controls, and rotating fixtures. These fixtures matter: a shadowed flute may receive uneven coverage. Small tools. Tight tolerances.

The coating process can use physical vapor deposition, or PVD, to apply materials such as titanium-based nitrides. Fraunhofer IST’s technical guidance places many PVD tool coatings around 1–5 micrometers thick. That thin layer can help reduce friction and wear without substantially changing a drill’s cutting geometry. The machine must control temperature, pressure, and tool movement. A few micrometers sound negligible, but on a micro drill, poor coverage or excess thickness can affect the cutting edge. ISO 20502 describes scratch testing for evaluating adhesion of ceramic coatings; it does not, by itself, prove a coating will perform well in every drilling setup. Actual results still depend on tool material, hole depth, feed rate, and workpiece. One detail is easy to overlook: a coating machine cannot compensate for a poorly prepared surface.

Typical Hardness Ranges of Coatings Used on Micro Drills

Representative coating hardness ranges in Vickers hardness (HV). Actual values vary with coating composition and deposition conditions.

Hard coatings can improve micro-drill wear resistance. When evaluating coating equipment, hardness is only one consideration; coating adhesion, thickness uniformity, process temperature, and substrate compatibility also matter.

How Hard Coating Improves Micro Drill Performance

A hard coating helps a micro drill resist abrasion, heat, and edge wear during repeated hole-making. That matters when a drill enters stainless steel and tiny chips struggle to escape its narrow flutes. A 2022 review of PVD cutting-tool coatings in Coatings reports typical TiAlN hardness in the range of about 3,000–3,500 HV. This hardness can protect the cutting edge, but it does not guarantee longer tool life. Coating adhesion, surface finish, and drilling conditions all matter.

Small details count. A thick coating can blunt a very fine cutting edge or reduce flute clearance. A thin, even layer is often more useful than maximum thickness. In practice, compare hole quality, burr formation, and tool wear across the same material and feed rate. The International Organization for Standardization’s ISO 513:2012 classification also shows why coating choice should match the workpiece and cutting conditions, rather than rely on hardness alone. Check the actual coating specification.

There is a trade-off. Higher cutting speeds may benefit from heat-resistant coatings, while poor chip evacuation can still break a micro drill quickly. A 2023 review in Surface and Coatings Technology notes that coating performance depends on both material properties and application conditions. That is easy to overlook. Suppliers should provide coating thickness, hardness-test method, and application guidance, not just a broad “wear-resistant” claim. Test a few tools first; real results can be less tidy than the catalogue.

Key Technologies and Machine Configurations

For micro-drill suppliers, coating capability depends on more than chamber size. A stable vacuum system helps control the deposition environment, while precise gas and power regulation supports repeatable film growth. Small details matter. Rotating fixtures can expose flute surfaces more evenly, especially when tools are densely loaded. For drills with very small diameters, fixture spacing and tool alignment deserve close attention. A crowded rack may reduce throughput, but it can also create uneven coverage.

Common configurations include batch vacuum chambers, programmable substrate rotation, temperature control, and process monitoring for pressure and deposition time. Some systems use arc evaporation; others use sputtering, with process choice depending on the coating material and tool requirements. Operators should check that loading methods protect fragile cutting edges and that recipes can be adjusted for different tool geometries. Even a well-designed setup may leave shadowed areas on complex flutes; that needs measurement, not assumption. Before selecting a machine, review sample-tool results, coating thickness data, and repeatability across multiple runs. A polished interface is useful, but it cannot replace process evidence.

How to Evaluate Micro Drill Coating Machine Suppliers

A micro drill coating machine supplier should understand the limits of small tools, not just describe a machine’s maximum capacity. Ask how the system controls coating thickness, temperature, and batch consistency across narrow flutes. Request sample process records and inspect whether measurements include the drill’s cutting edges, not only a flat test coupon. Small details matter. A few microns can affect tool life, chip evacuation, and hole quality.

Check whether the supplier can run a trial with your actual drill material, diameter, and coating target. Compare tools before and after treatment under the same cutting conditions, then review wear patterns and hole measurements. Ask about fixture design, chamber loading, maintenance intervals, and operator training; these practical details can shape results as much as the coating process itself. Run a trial. Notice how clearly technical questions are answered, and whether limitations are stated plainly. A polished presentation is useful, but it is not proof of repeatability. If test data is incomplete, pause and ask what was measured, how many tools were tested, and whether the results reflect normal production. That extra check may feel slow, but skipping it can be costly.

Leading Micro Drill Hard Coating Machine Suppliers in 2026

Leading Micro Drill Hard Coating Machine Suppliers in 2026

Choosing a micro drill hard coating machine supplier is less about a polished brochure and more about repeatable results on tiny tools. Ask how the system controls temperature, coating thickness, and batch uniformity. A few microns matter. Suppliers should provide process records and practical trials using your drill material, geometry, and cutting conditions. Inspect flute edges under magnification; coating buildup can affect chip evacuation and hole quality.

Automation raises the stakes. The International Federation of Robotics reported 4,281,585 industrial robots operating worldwide in 2023, a 10% increase from 2022, in its World Robotics 2024 report. That figure does not measure coating demand directly, but it shows how production lines increasingly depend on consistent tooling. A capable supplier should explain chamber loading, fixturing, cycle time, and maintenance—not just quote peak capacity. Tiny tools punish inconsistency.

Compare suppliers using sample results, service response, and documented process windows. Request coating-thickness measurements across several drills, plus adhesion and wear-test methods. The ISO 13399 cutting-tool data standard also offers a useful framework for clear tool information, though it does not certify coating performance. One awkward truth: a successful trial on one drill size proves little about another. Ask for repeat tests, and keep the results.

2026 Top Micro Drill Hard Coating Machine Suppliers - Leading Micro Drill Hard Coating Machine Suppliers in 2026 Supplier evaluation benchmarks for micro-drill hard-coating equipment and coating services
Evaluation Dimension Technical Reference or Benchmark What Buyers Should Verify
Coating process Physical vapor deposition (PVD) is commonly used for hard coatings on cutting tools. Available processes and coating chemistries vary by equipment configuration. Confirm the process type, supported coating materials, batch configuration, and whether the system is designed for small cutting tools.
Micro-drill diameter scope Micro-drill usage commonly includes tools below approximately 3 mm in diameter; the precise definition varies by application and market. Request the supplier’s minimum and maximum tool diameters, fixture drawings, and examples using tools comparable to the intended drill geometry.
Coating thickness Hard-coating thicknesses around 1–3 μm are a common reference range for cutting tools. The suitable value depends on tool size, geometry, substrate, and application. Specify the target thickness and tolerance. Ask how thickness is measured and how uniformity is checked on flutes, cutting edges, and recessed areas.
Coating temperature PVD tool-coating temperatures depend on the process and coating recipe. Lower-temperature options may be important for temperature-sensitive substrates or tool treatments. Obtain the process temperature range and confirm that it is compatible with the drill substrate, brazing or joining materials, and existing heat treatment.
Coating options Common hard-coating families for cutting tools include titanium nitride (TiN), titanium aluminum nitride (TiAlN), and chromium-based nitride coatings. Selection depends on workpiece material and cutting conditions. Ask for the coating composition, intended application, and test data for the specific workpiece material and machining conditions.
Edge and flute coverage Small drill features make coating distribution and preservation of cutting geometry important. Results depend on part orientation, fixturing, and process setup. Review sample tools under magnification and request coating-distribution data from representative cutting edges and flute locations.
Adhesion and quality testing Adhesion, thickness, surface condition, and coating defects are relevant quality checks. Test methods should be appropriate to the tool geometry and coating system. Request documented inspection methods, acceptance criteria, batch traceability, and sample test reports.
Tool performance validation Coating performance is application-specific; tool life and wear depend on substrate, drill geometry, workpiece, coolant, and cutting parameters. Compare coated and uncoated drills in a controlled trial using the same machining conditions and an agreed tool-life or wear criterion.
Equipment and service capability Equipment suppliers and coating-service providers may offer different combinations of process development, production coating, maintenance, and technical support. Confirm whether the supplier sells equipment, provides coating services, or both; also verify installation, operator training, spare parts, and maintenance support.
Supplier qualification No single coating specification is suitable for every micro-drilling application; qualification should be based on documented requirements and representative trials. Evaluate sample quality, process consistency, technical documentation, delivery terms, and the supplier’s ability to reproduce agreed results.
Note: The technical ranges and examples above are general industry references, not claims about any specific supplier. Confirm specifications and performance with the supplier for the intended tool and application.